Key Takeaways
- CNC machining reduces avoidable waste when programming, stock selection, tooling, and inspection are planned together.
- Scrap can result from setup errors, tool wear, unstable clamping, incorrect cutting conditions, or incomplete design information.
- First-piece inspection and in-process checks help prevent a small error from affecting an entire batch.
- Tracking rework, cycle time, tool changes, and material yield helps teams find process issues that a simple scrap count can miss.
For manufacturers across Dallas, Texas, controlling material use is an important part of managing production costs, lead times, and part consistency. A CNC machine shop can support this effort by turning digital designs into repeatable cutting instructions, but strong results still depend on decisions made before and during production.
Dallas-area production teams often balance short turnaround expectations with the need to meet precise drawing requirements. That makes process control especially valuable. A rushed setup, an overlooked fixture issue, or excess stock allowance can create chips, offcuts, rework, and schedule disruption that could have been prevented earlier.
Why Material Waste Still Matters in CNC Machining
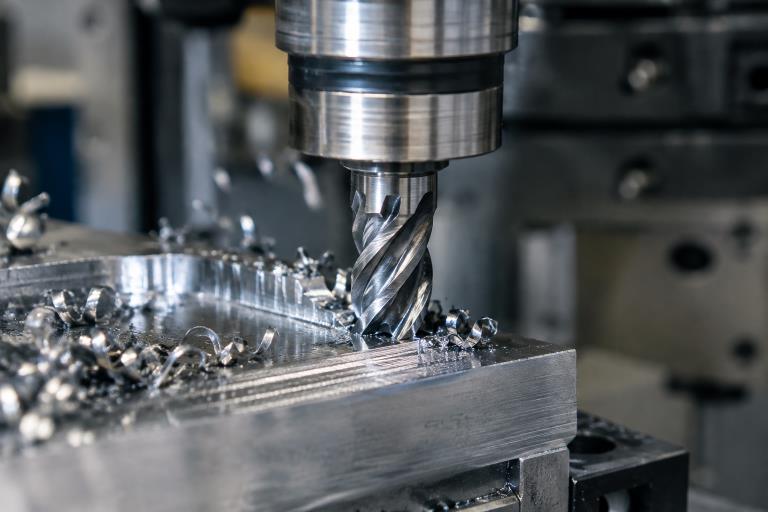
CNC machining is a subtractive process, meaning a cutter removes material from a solid workpiece to create the finished part. Some chips and trim are expected. Avoidable waste is different. It includes parts rejected due to incorrect dimensions, poor surface finish, damage during clamping, programming errors, or cutting tools used beyond their effective life.
The cost of a scrapped part is not limited to the raw metal or plastic. It can also include machine time, labor, tooling, inspection effort, replacement material, and delayed downstream work. Reducing material at the source aligns with the broader principle of reducing, reusing, and recycling materials before treating disposal as the primary option.
For projects that move between North Texas and other major Texas manufacturing markets, CNC machining provides a structured way to produce prototypes, replacement components, and recurring production parts. The process is most efficient when the part design and manufacturing plan account for the realities of cutting, measuring, and securely holding the material.
How Programming Supports Better Material Use
CAD software defines the part geometry, while CAM software helps translate that geometry into toolpaths and machine instructions. A programmer must consider more than the finished shape. Stock dimensions, workholding locations, tool access, cutting direction, finishing allowance, and safe clearance moves all affect the outcome.
For example, a poorly planned plate layout may leave large unusable spaces between parts. Revising the layout, material orientation, or toolpath order may improve stock utilization. Program simulation is also useful because it can reveal collisions, wasted machine movement, and excessive material removal before an operator commits material to the machine.
Five Ways to Reduce Scrap
- Review the part design. Deep pockets, very thin walls, sharp internal corners, and difficult-to-reach features can raise machining risk. Early design review can identify features that need a different radius, tool approach, or sequence.
- Select suitable stock. Oversized stock increases cutting time and chip volume, while undersized stock may leave too little material for required features.
- Use stable workholding. Fixtures and clamps must locate the workpiece consistently without allowing vibration or distortion.
- Match cutting conditions to the job. Feed rate, spindle speed, depth of cut, coolant strategy, tool material, and workpiece material need to work together.
- Inspect the first piece. Checking critical features before running the rest of a batch limits the impact of setup or programming errors.
Tooling, Fixtures, and Setup Control
Tool selection affects both surface finish and dimensional accuracy. Tool diameter, geometry, coating, and material influence how a cutter removes material. As a tool wears, operators may see burrs, chatter, inconsistent finishes, or dimensional drift. Keeping tool-life records can help a team replace tools based on observed performance rather than waiting for a visible failure.
Fixtures deserve the same attention. Uneven clamping pressure, poor alignment, and limited tool access can turn a correct program into a failed part. Thin or flexible workpieces are especially susceptible to deflection during machining. Clear setup documentation should include workholding photos, datum locations, tool lists, torque or clamping guidance where applicable, and required inspection points.
Inspection Should Prevent Rework, Not Only Document It
First-article inspection verifies the initial completed part. In-process inspection checks selected features while production continues, and final inspection confirms that finished parts meet the specified requirements. Depending on the job, teams may use probes, gauges, micrometers, calipers, coordinate measuring machines, or surface-finish instruments.
Inspection data can reveal a gradual change before it becomes a rejection problem. For instance, repeated movement toward a tolerance limit may indicate tool wear, thermal change, fixture movement, or machine drift. Research into sensor-based condition monitoring also shows how machine and tool data can help identify wear or potential failures earlier in the machining process.
Using Data to Find Hidden Process Waste
A scrap total is useful, but it does not explain why parts failed. Dallas manufacturers can gain a clearer picture by reviewing a small set of repeatable process measures, including:
- Scrap rate by part number and operation
- Rework hours and the reason for rework
- Actual cycle time compared with planned cycle time
- Average setup time and tool changes per batch
- Material yield, machine idle time, and first-pass yield
A pattern in this data may point to a design concern, a programming issue, a fixture weakness, inconsistent cutting conditions, or an inspection gap. Reviewing the cause is more useful than treating every rejected part as an isolated event.
Where Automation and Digital Tools Fit In
Automation does not replace careful planning, but it can make a stable process easier to repeat. Tool measurement, probing, pallet systems, robotic loading, machine monitoring, and machining simulation can reduce manual variation and provide earlier warning when a cycle changes. Digital models can also help teams test toolpaths and workholding concepts before production begins.
A Practical Workflow for Lower-Waste Production
- Review the drawing, model, material, tolerances, and surface-finish requirements.
- Identify difficult features and select stock, tools, fixtures, and cutting conditions.
- Simulate the program and verify clearance, tool access, and material removal.
- Run and inspect a controlled first piece before continuing the batch.
- Record cycle time, tool condition, inspection findings, and material use.
- Update the setup or program when the results show an opportunity to improve.
Better Machining Starts With Better Process Control
Lower-waste CNC production is rarely the result of a single technology purchase or an isolated adjustment. It comes from integrating design review, programming, stock selection, tooling, workholding, inspection, and data review into a single disciplined process. When each step supports the next, Dallas manufacturers can reduce avoidable scrap while improving consistency from the first part through the final run.